Key Takeaways
- Bullet ice, diamond ice golf balls, and standard tray cubes solve three different problems: fitting narrow bottle openings, slowing dilution in a glass, and producing volume for everyday use.
- Silicone is the default material for shaped novelty ice because flexible cavity walls release undercut geometries that rigid trays cannot demold cleanly.
- Most "ice maker silicon tray" searches are really design questions: cavity geometry, fill line, lid fit, wall thickness, and water expansion matter more than the material name alone.
- Custom ice mold projects follow a predictable path — design review, sample, tooling, production, inspection, packaging — and MOQ, mold fees, and lead times should always be quoted per project rather than assumed.
- Buyers should confirm current availability, material composition, dimensions, compliance documentation, MOQ, and lead time for their specific market before publishing product specifications.
1. Introduction
Ice is one of the cheapest things in a kitchen and one of the easiest to get wrong. A round ice ball that looks striking in a whiskey glass can be a nightmare to release from a cheap tray. A long bullet-shaped cylinder that slides perfectly into a sports bottle will not fit a rocks glass. A standard cube tray is unglamorous but freezes more usable ice per shelf than almost any novelty mold.
That gap between how ice looks and how it performs is why searches for fun ice cube mold trays rarely end with a simple purchase. Buyers — whether a home bartender, a gift shop owner, a promotional-products distributor, or a brand planning a private-label launch — usually arrive with a shape in mind and a set of unanswered questions behind it: Will it demold cleanly? Will the ball crack in the freezer? Why does the tray smell like last month's garlic? What is a realistic minimum order quantity?
This article breaks the category into its three most common formats — bullet ice molds, diamond ice golf balls, and tray ice — and explains what each is actually good for, how silicone changes the design rules, and how a custom mold project moves from a sketch to a shipment. It is written for readers who need to compare formats or brief a supplier, not just browse pictures.
2. Bullet Ice Molds, Diamond Ice Golf Balls, and Tray Ice: Three Formats, Three Jobs
Core conclusion: these three formats are not interchangeable upgrades of one another. Choose the format from the glass or container it will go into, then choose the mold from the demolding difficulty of that shape.
Bullet ice molds produce elongated cylinders with rounded ends. Their practical advantage is dimensional: a narrow-diameter cylinder enters bottle necks, carafes, and insulated flasks that reject a wide cube. The trade-off is freeze time. A thick cylinder has a low surface-area-to-volume ratio, so the center takes noticeably longer to become solid than a small cube does — and partially frozen bullet ice tends to crack or shear when it is released. Bullet molds therefore benefit from long, straight cavities with generous draft and a flexible wall that can peel away from the length of the shape rather than gripping it.
Diamond ice golf balls are spheres or near-spheres with a faceted, gem-like surface pattern. The geometry serves a clear purpose in a glass: a compact sphere exposes less surface area per unit volume than a cluster of small cubes, so it melts more slowly and dilutes a drink more gradually. The pattern is decorative, but it also creates texture that helps the ball release from a multi-part cavity. Spheres are the hardest of the three formats to mold well, because the cavity has no natural draft direction and the water inside expands roughly nine percent by volume as it freezes. Fill lines and cavity headspace have to be designed around that expansion.
Tray ice — the classic grid of cubes or the block-style "ice block molds" used for large slabs — wins on throughput. A flat tray uses freezer shelf area efficiently, stacks well with a lid, and produces ice that works in almost any vessel. Its limitation is purely aesthetic and functional: cubes dilute faster than a large sphere, and standard grids cannot produce a shape that a brand would want to print on.
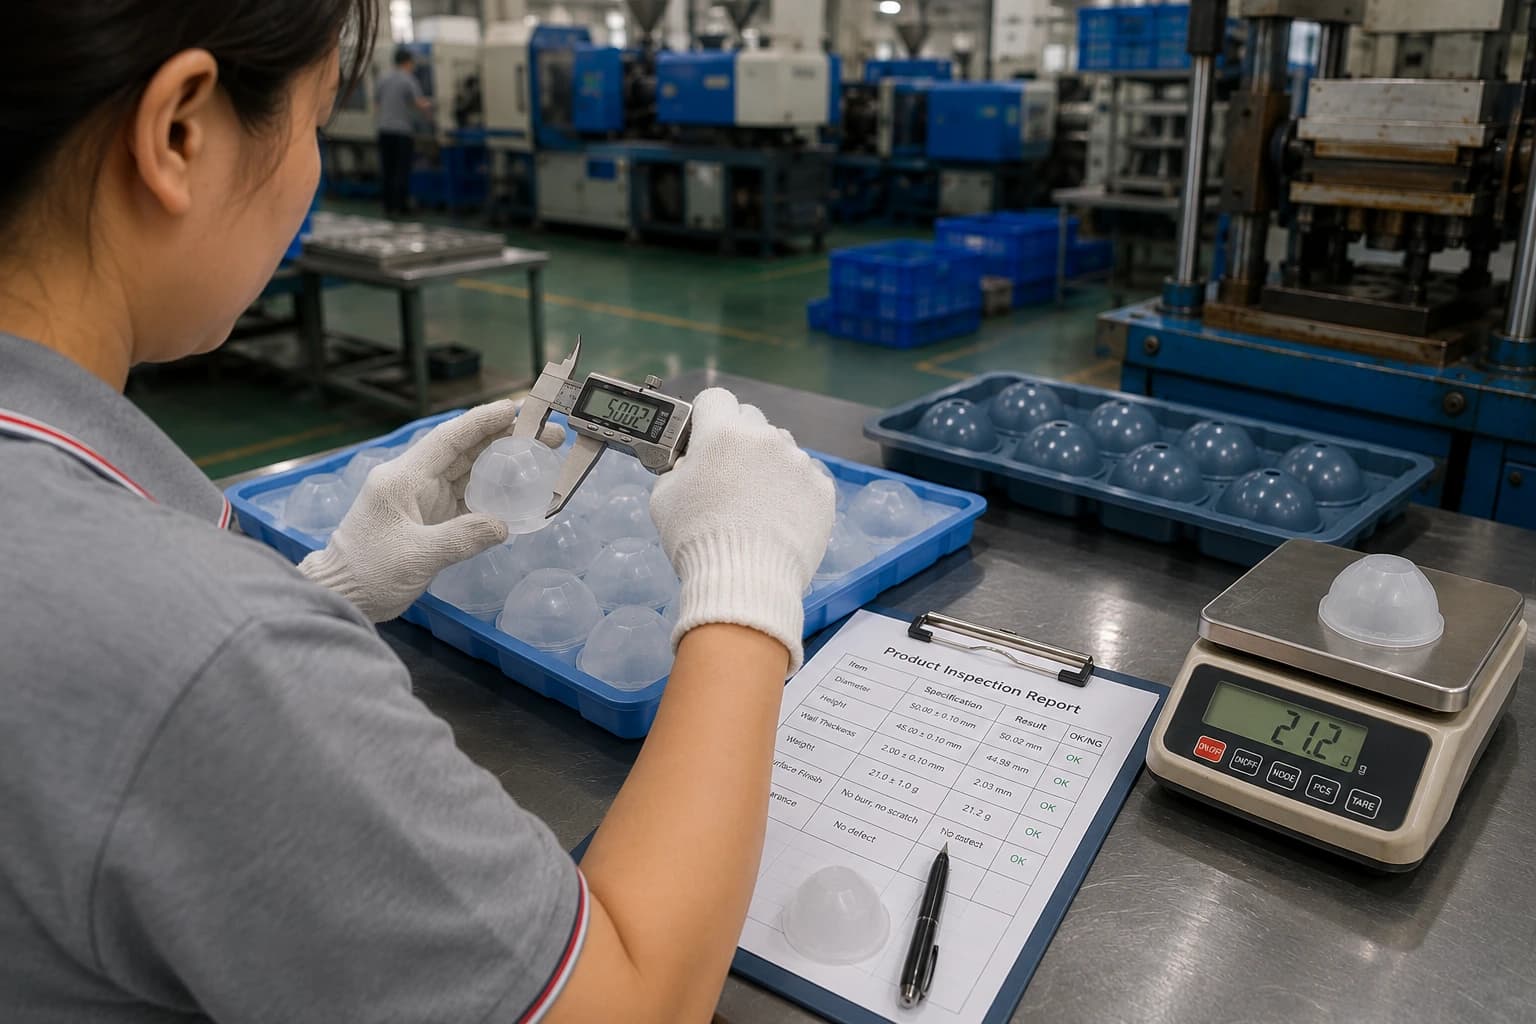
Ice molds are often filed under household, kitchen, or promotional product lines depending on the sales channel, and that category placement should not restrict how you think about the format [K4]. A bullet mold sold as a household item and the same mold sold as a branded promotional gift are the same engineering problem.
| Format | Shape | Best for | Mold difficulty | Main design risk |
|---|---|---|---|---|
| Bullet ice | Rounded cylinder | Bottles, flasks, carafes, pitchers | Moderate | Partial freezing and cracking in thick sections |
| Diamond ice golf ball | Faceted sphere | Whiskey, cocktails, slow-dilution serves | High (multi-part cavity) | Fill line and expansion headspace |
| Tray ice | Cube grid or block | Everyday volume, coolers, batch use | Low | Lid fit and stacking stability |
Practical advice: if a buyer only needs ice that fits a bottle, a bullet mold is the shortest path. If the product is a gift or a branded item where the visual moment matters, the diamond ball justifies its higher tooling complexity. If the goal is volume, do not over-engineer — buy a tray.
3. Why Silicone Is the Default Material for Novelty Ice — and Where It Stops
Core conclusion: silicone is chosen for shaped ice mainly because it is flexible, not because it freezes faster. Understanding that trade-off prevents most demolding complaints.
A rigid plastic or metal tray relies on the ice releasing itself: the cube shrinks slightly, and a twist or a warm-water dip breaks the bond. That works for simple tapered cubes and fails for anything with an undercut, a narrow neck, or a faceted surface. A flexible cavity can be peeled back from the ice, so the shape can be more adventurous — which is exactly why most novelty formats ship as silicone.
Two practical consequences follow.
First, silicone is a comparatively poor heat conductor. An aluminum tray will generally pull heat out of water faster than a thick silicone wall, so a silicone mold usually needs more freezer time for the same ice volume. That is a fair trade for demolding flexibility, but it means the mold's wall thickness is a real design decision, not a cosmetic one. Thin, even walls freeze faster and still release cleanly; overly thick walls add mass without adding function.
Second, flexibility does not fix a bad cavity. A sphere with no expansion headspace will still crack. A bullet cavity that is too deep and too narrow will still hold its ice. When a shopper searches for an ice maker silicon tray, what they usually want is a tray that releases without a fight — and that outcome comes from cavity design, draft, fill line marking, and lid geometry more than from the word "silicone" on the box.
Material specification also deserves more scrutiny than it often gets. Cure system, hardness, and clarity affect how a mold feels in the hand, how easily it releases, and whether it retains odors over time. Those attributes should be confirmed against a written specification for the actual product rather than inferred from a category description, and buyers preparing a private-label program should treat material confirmation as a formal step in the sourcing process [K4].
Practical advice: store silicone trays dry, empty, and away from prolonged contact with strongly scented foods, and use the lid where one is supplied. If a mold develops a persistent smell, the cause is usually storage and residue rather than the material itself — a hot-water wash and thorough drying resolves most cases. For branded or private-label programs, work through a supplier's silicone OEM/ODM development process so that hardness, color, and packaging are specified together rather than negotiated piecemeal.
4. From Design File to Production: How a Custom Ice Mold Project Actually Runs
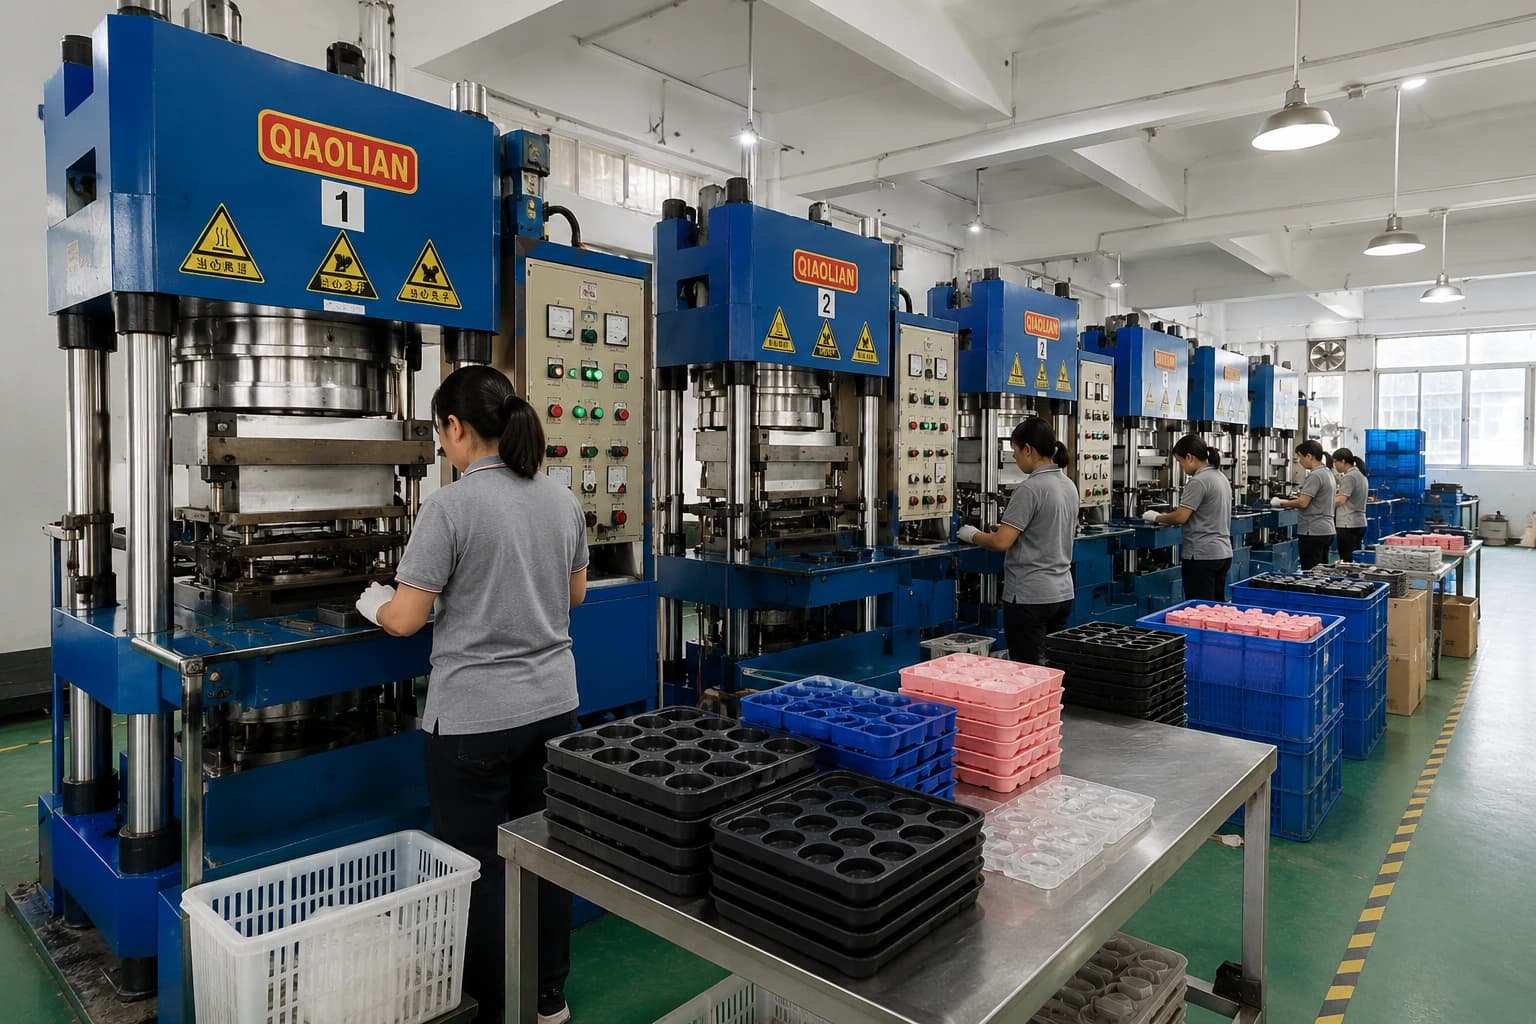
Core conclusion: a custom ice mold is a small tooling project with a fixed sequence. Skipping the sample stage is the most expensive shortcut available.
Custom silicone ice molds are typically customized across cavity design, product shape, size, color, logo, and packaging [K1]. That list looks short but each item has a dependency: changing the cavity shape reopens the tooling question, changing the color affects minimum batch planning, and adding a logo to the mold body or the packaging changes the sampling requirement.
The sequence that reliably works looks like this:
- Design review. The buyer supplies the intended use (glass type, bottle neck diameter, target ice volume), plus any brand assets. The supplier checks whether the geometry is moldable in silicone as drawn.
- Design-file preparation. Artwork, dimensions, cavity layout, and packaging dielines are consolidated into a production-ready specification.
- Tooling. A mold is cut or machined from the approved geometry. Mold fees depend on cavity complexity and should never be quoted as a fixed number before design evaluation [K5].
- Sampling. Physical samples are produced and reviewed for release behavior, fill line, lid fit, weight, and finish.
- Approval and production. Only after written sample approval should bulk production be scheduled.
- Inspection and packaging. Pre-shipment checks cover cavity consistency, color match, and packaging integrity.
This workflow is standard for silicone OEM/ODM work, and the same pattern applies whether the product is an ice mold, a promotional silicone product such as a branded ice cube tray, or a popsicle mold from an adjacent product line [K2]. The reason to describe it in stages is accountability: each stage produces a document or a physical object that both sides can point to later.
Practical advice: approve samples against a written checklist, not against a photograph. Confirm the fill line is visible, that the ball or bullet releases without tearing, that the lid seats without force, and that the packed unit survives a drop test in its retail packaging. Ask for the sample to be produced from the same tooling that will run production — a sample from a machined prototype proves the shape, not the process.
5. Sourcing Boundaries: MOQ, Tooling, Lead Time, and Compliance Claims
Core conclusion: treat MOQ, mold cost, sample cost, freight, and lead time as project-specific variables, and treat certification language as something to verify rather than assert.
Several assumptions circulate in this category and cause avoidable friction later:
- MOQ. There is no universal minimum that applies to every custom project. A simple single-cavity tray and a multi-part faceted sphere mold carry very different setup economics. Any supplier who quotes one number across all projects is simplifying — and buyers who repeat that number publicly may be overstating what was actually agreed [K5].
- Samples and freight. Free samples and free freight are commercial decisions, not category standards. They should be confirmed in writing per project [K5].
- Dates. Sampling, tooling, and production timelines depend on design review and written confirmation. A date given verbally during an inquiry is an estimate, not a commitment [K5].
- Mold fees. A mold fee cannot be published as fixed before the design has been evaluated, because cavity count and geometry drive the cost [K5].
- Compliance. Food-contact requirements differ by market, and the correct approach is market-specific compliance planning based on documentation for the actual product — not blanket certification claims copied from a listing [K3]. Buyers should request the specific test reports and declarations relevant to their destination market and confirm material composition per product [K4].
Practical advice: build a one-page specification sheet for every ice mold SKU — shape, cavity count, nominal ice volume, material, hardness, color reference, packaging format, and destination market. Send that sheet with every inquiry. It shortens design review and prevents the most common source of rework, which is a supplier building to an assumption.
6. Buyer Checklist: Comparing Formats and Vendors
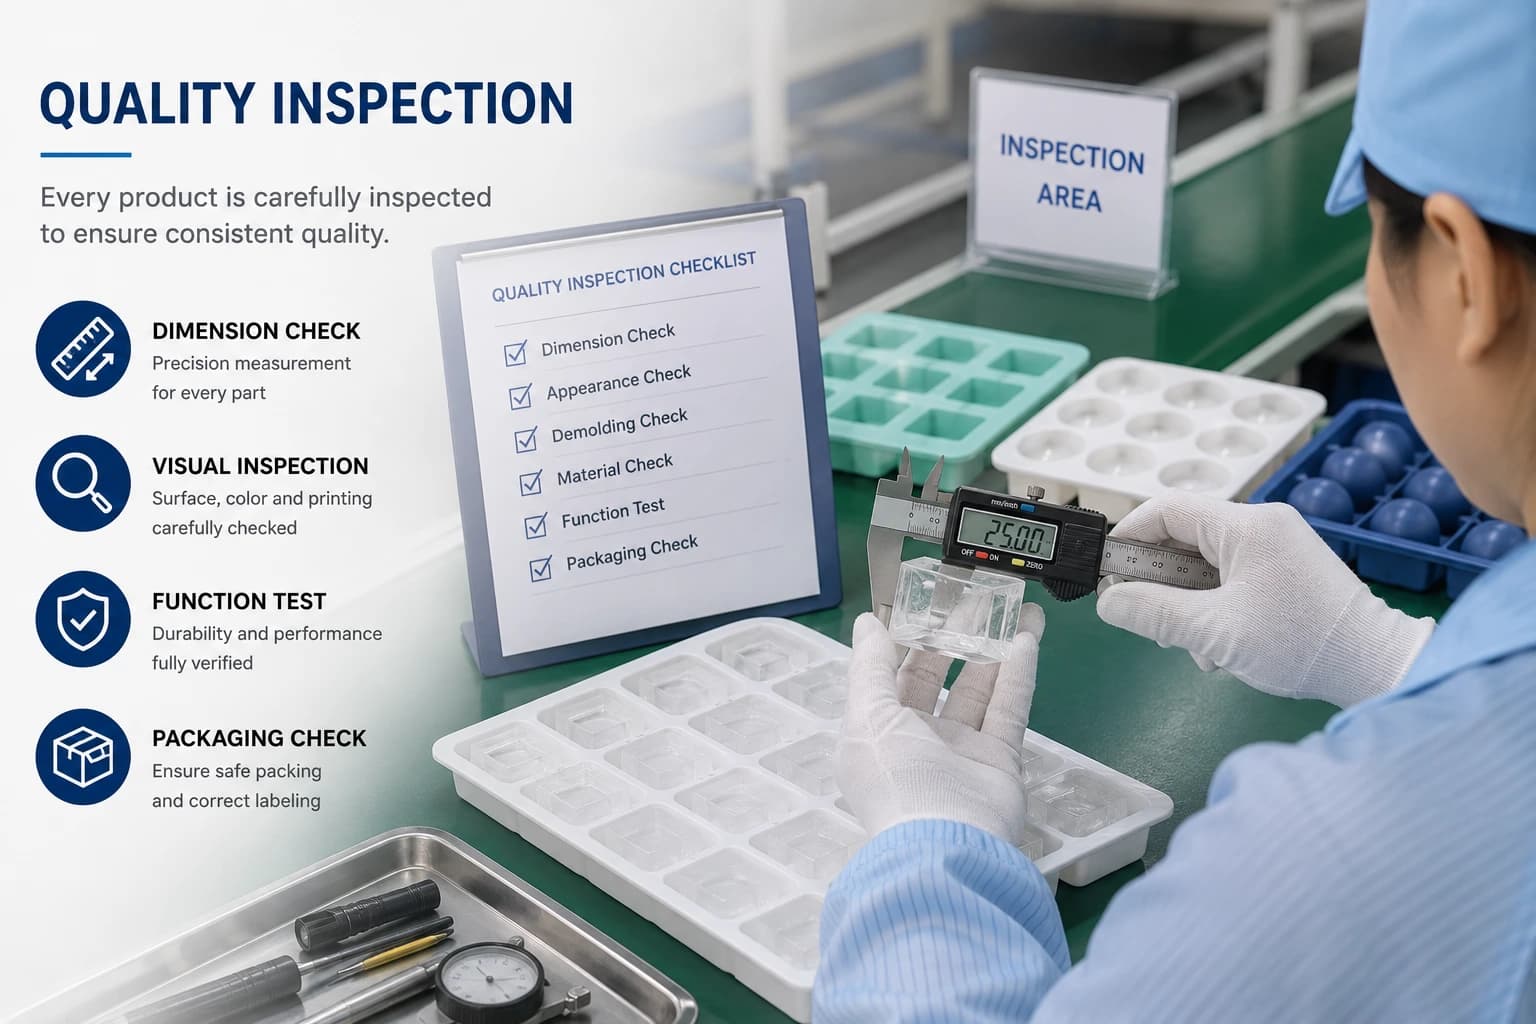
Before committing to a format or a supplier, verify the items below. Each one maps to a decision that is expensive to reverse after tooling.
| Check | Why it matters | When to verify |
|---|---|---|
| Intended vessel fit (neck diameter, glass width) | Determines whether bullet, ball, or cube format is viable | Before design review |
| Ice volume per cavity and per cycle | Sets expectations for freeze time and yield | Before tooling |
| Fill line and expansion headspace | Prevents cracked spheres and stressed bullets | At sample stage |
| Demolding behavior | The single most common end-user complaint | At sample stage |
| Lid fit and stacking stability | Affects freezer usability and retail packaging | At sample stage |
| Material specification (hardness, cure, color) | Affects feel, release, and odor retention | Before sampling |
| Current availability and dimensions | Portfolio listings are not a stock guarantee | Before publishing specs [K4] |
| MOQ, mold fee, sample cost, freight terms | Project-specific; must be in writing | Before quotation [K5] |
| Lead time with written confirmation | Verbal estimates are not commitments | Before purchase order [K5] |
| Market-specific compliance documents | Requirements vary by destination | Before shipment [K3] |
The comparison logic is simple. Bullet ice wins on container compatibility, diamond golf balls win on presentation and slow dilution, and tray ice wins on volume and cost per usable cube. Within any of those formats, the difference between a mold that delights and one that frustrates is almost always the sample stage — not the marketing copy.
7. FAQ
Q1. Can one silicone mold produce both bullet ice and ice balls?
Not usually from the same cavity. Bullet cavities are long and directional; sphere cavities need expansion headspace in multiple directions and often a two-part or split design. A single tray can carry two different cavity sets, but each cavity still needs its own geometry review, and the tooling cost reflects the combined complexity.
Q2. Why does my ice ball crack in the freezer?
Cracking is nearly always an expansion problem. Water expands as it freezes, and a sphere has no natural direction to relieve that pressure if the cavity is filled too high or lacks headspace. Fill to the marked line, leave the headspace the mold was designed for, and avoid stacking heavy items on a filled tray.
Q3. Is a lower MOQ always the better deal?
No. A low MOQ reduces inventory risk, but per-unit cost is usually higher because tooling and setup are spread across fewer units. The right question is how many units you can realistically sell or distribute before the design needs revision — then negotiate MOQ against that number, with the understanding that any figure is project-specific and should be confirmed in writing rather than assumed [K5].
Q4. How do I know whether a quoted ice mold is actually silicone?
Ask for the material specification for that specific product, including hardness and cure system, and confirm it against the sample you receive. Category-level descriptions are not a substitute for a product-level specification, and material composition should be confirmed per item before any public claim is made [K4].
8. Conclusion
The three formats in this category are tools with different jobs. Bullet ice molds solve fit — they get ice into narrow openings that reject cubes. Diamond ice golf balls solve presentation and dilution — the compact faceted sphere melts slowly and looks deliberate in the glass. Tray ice solves volume — it produces more usable ice per shelf with the least fuss. Choosing well starts with the vessel and the occasion, not with the shape that photographs best.
For buyers moving beyond retail purchases into private label, the decision shifts from format to process. Confirm the geometry is moldable in silicone, approve a physical sample against a written checklist, and treat MOQ, mold cost, sample terms, lead times, and compliance documentation as project-specific items that must be confirmed in writing rather than inherited from a category assumption [K3][K5]. A fun ice mold is a small product, but it is still tooling — and the projects that go smoothly are the ones that spent their time on the sample stage instead of the quotation.